Your CMMS already contains the data that could predict your next electric motor failure in the steel plant — the problem is that 89% of steel mill maintenance teams never analyze it for predictive patterns. Every motor current waveform your electricians have recorded, every vibration reading your condition monitoring team has logged, every unexpected shutdown your operators have reported over the past 24 months contains failure signatures that repeat with statistical regularity across motor types, load conditions, and operating cycles. A 2025 International Journal of Electrical and Electronics Research study found that multi-resolution current signature analysis achieves significantly better accuracy in induction motor fault prognosis — not by installing expensive new sensors or AI platforms, but by systematically analyzing the current signals already available from existing motor protection relays and VFDs [citation:1]. The rotor bar that fails at 18 months on your roughing mill motor is not a random event — it is the third rotor bar failure on that motor class in your plant this year, and the previous two showed the characteristic sideband pattern at 2sf (twice slip frequency) weeks before failure. That pattern is sitting in your motor data right now, invisible because nobody has built the analysis workflow that surfaces it. Oxmaint's motor condition monitoring module turns your existing current signature data into a failure prediction engine — automatically extracting harmonic patterns, flagging sideband amplitudes exceeding thresholds, and generating preventive work orders before the motor fails. The data is already yours, and the analysis that prevents the next unplanned motor replacement takes minutes to configure, not months. If your steel plant is still reacting to motor failures instead of predicting them from the current signature data you already collect, start a free trial or book a demo to see how Oxmaint surfaces motor fault patterns from your existing data.
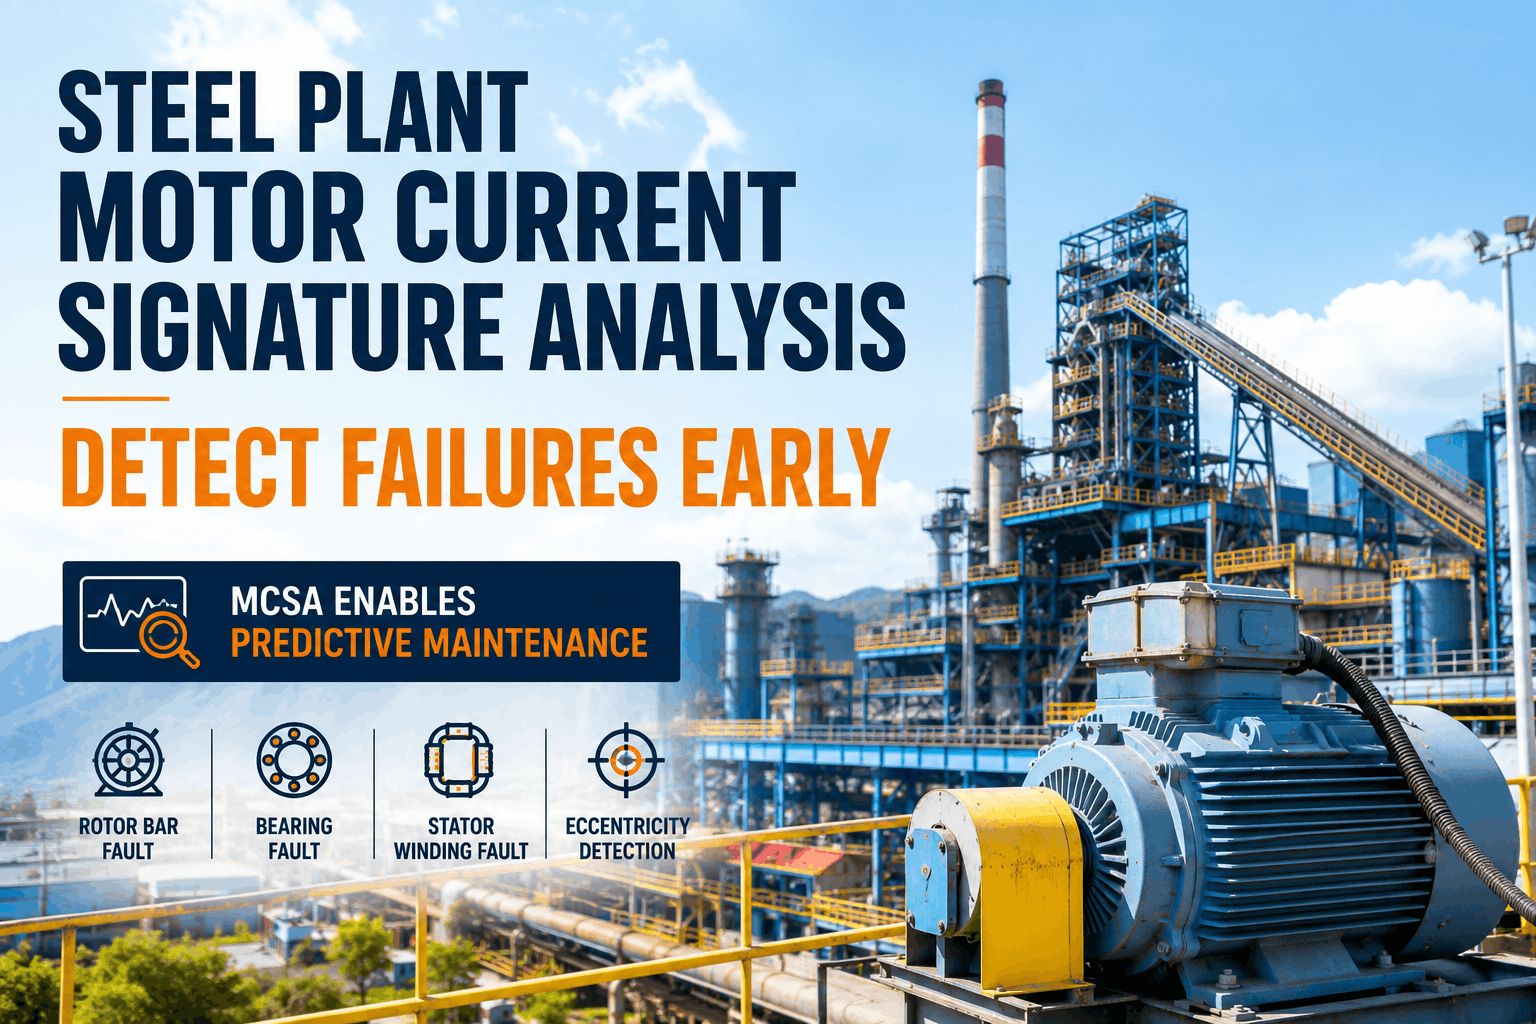
Steel Plant Predictive Maintenance for Electric Motors: Current Signature Analysis
Motor current signature analysis (MCSA) for predictive maintenance of steel plant motors — detecting rotor bar defects, stator winding faults, bearing faults, and eccentricity before catastrophic failure occurs.
You Already Have the Current Data — You Just Need the Analysis
Every motor current waveform captured by your protection relays, VFDs, or portable data collectors is a diagnostic data point. Every harmonic sideband is a fault signature. Every amplitude variation is a wear indicator. MCSA does not require new sensors or expensive condition monitoring hardware — it analyzes the current signals already available from existing instrumentation and surfaces the patterns that predict failure. Steel plants with 50 or more motors can start a free trial or book a demo to see how current signature analysis works on your plant's motor data.
What Is Motor Current Signature Analysis for Predictive Maintenance?
Motor Current Signature Analysis (MCSA) is a non-invasive condition-monitoring technique that detects mechanical and electrical faults in electric motors by analyzing the harmonic content of stator-current signals [citation:2]. Unlike vibration monitoring or thermal imaging, MCSA does not require expensive specialized sensors or physical access to the motor. The current signal is acquired from one phase of the motor supply at the motor terminal box or local electrical panel without interrupting machine operation [citation:3].
The core principle is simple: when a motor is healthy, its current frequency spectrum shows a dominant peak at the supply frequency (50Hz or 60Hz). When faults develop — broken rotor bars, stator winding shorts, bearing defects, or eccentricity — characteristic sideband frequencies appear around the supply frequency and its harmonics [citation:3]. These sideband frequencies are directly related to the motor's physical characteristics: rotor bar count, pole-pair number, slip frequency, and mechanical rotational speed. The amplitude of these sidebands relative to the supply frequency provides a quantitative measure of fault severity, enabling detection of incipient failures before they become catastrophic.
The Four Fault Categories MCSA Detects in Steel Plant Motors
MCSA can detect four distinct categories of motor faults, each with unique spectral signatures. When analyzed over time, these signatures reveal failure progression and enable predictive maintenance scheduling [citation:3].
Four Eccentricity and Fault Patterns Your Current Data Will Reveal
When you analyze current spectra over time, four distinct eccentricity and fault patterns emerge. Each pattern type has a different maintenance response — and each is invisible until the spectral analysis is performed [citation:3].
Static eccentricity occurs when the rotor's geometrical and rotational centers are identical but different from the stator center. The point of minimal air-gap length is stationary with respect to the stator. Caused by manufacturing tolerances between the stator bore and bearing centers. Your current spectra reveal static eccentricity as sidebands at frequencies fd = fg ± (R/p)(1-s)fg where R is rotor bar count and p is pole-pairs [citation:3].
Dynamic eccentricity occurs when the rotor's geometrical center differs from the rotational center. The point of minimal air-gap moves with rotor rotation. This pattern indicates bearing wear, shaft deflection, or rotor imbalance. Your current spectra reveal dynamic eccentricity through additional modulation of static eccentricity frequencies with the rotational frequency fr [citation:3].
Mixed eccentricity combines both static and dynamic effects — rotor and rotational centers are different from the stator center. This pattern is common in older steel plant motors with accumulated wear. Your current spectra reveal mixed eccentricity through combined sideband patterns that require advanced spectral analysis to separate [citation:3].
Steel plants increasingly use variable frequency drives (VFDs) for energy efficiency. However, VFDs introduce harmonics that can mask fault signatures. Your current data analysis must account for VFD carrier frequencies and switching harmonics to avoid false positives. Advanced algorithms with notch filtering or empirical wavelet transform separate VFD artifacts from actual fault signatures [citation:1][citation:2].
How Oxmaint Turns Motor Current Data Into Failure Prediction
Oxmaint's motor condition monitoring module is not a standalone spectral analysis tool bolted onto your maintenance process — it is the CMMS that collects motor data, structures it correctly, and surfaces fault patterns automatically as part of daily steel plant operations. Every current waveform, every spectral peak, every sideband amplitude feeds the prediction engine without any additional data entry. Steel plants ready to move from reactive to predictive motor maintenance can start a free trial or book a demo to see the MCSA workflow on live plant data.
Oxmaint integrates with existing motor protection relays, VFDs, and portable data collectors. Current signals are captured from one phase at the motor terminal box or electrical panel without interrupting operation. Standard file formats supported: CSV, WAV, NumPy arrays [citation:2].
Oxmaint performs complete spectral analysis including FFT for harmonic content, Welch PSD for power spectral density, and automated peak detection to identify fault sidebands [citation:2]. Preprocessing includes DC removal, windowing, and filtering.
Oxmaint's fault pattern library automatically detects broken rotor bars, air-gap eccentricity, stator inter-turn short circuits, and bearing defects. Fault indices are computed from sideband amplitude ratios relative to the supply fundamental [citation:2].
Faults are classified into four severity levels — healthy, incipient, moderate, severe — based on thresholds from peer-reviewed literature and international standards [citation:2]. This enables appropriate maintenance response: continue monitoring, schedule inspection, plan repair, or immediate replacement.
Oxmaint stores historical spectral data and tracks fault amplitude trends over time. This enables prediction of remaining useful life and scheduling of preventive maintenance before failure occurs. Advanced multi-resolution analysis extracts features for artificial neural network-based prognosis [citation:1].
When fault severity reaches predefined thresholds, Oxmaint automatically generates preventive work orders with detailed fault analysis, recommended actions, and supporting spectral data attached for the maintenance technician. This ensures the right response at the right time.
Reactive Motor Maintenance vs MCSA-Driven Prediction
Key Fault Frequencies for Steel Plant Motor Diagnosis
The table below provides the key fault frequencies for MCSA diagnosis in steel plant motors. These frequencies are calculated based on motor characteristics and operating conditions [citation:3].
| Fault Type | Fault Frequency | Variables | Steel Plant Application |
|---|---|---|---|
| Broken Rotor Bars | fb = f1(1±2s) | f1 = supply frequency, s = slip (per unit) | Rolling mill motors, conveyor drives |
| Bearing Defects | f0 = 0.4 frm, f1 = 0.6 frm | frm = rotor mechanical frequency | All motors with rolling element bearings |
| Static Eccentricity | fec = fg ± (R/p)(1-s)fg | R = rotor bar count, p = pole-pairs, s = slip | High-speed induction motors |
| Dynamic Eccentricity | fec = fg ± fr with additional modulation | fr = rotational frequency | Motors with bearing wear or shaft deflection |
| Stator Winding Shorts | Harmonics above 2f1 (25Hz, 75Hz at no-load) | f1 = supply frequency | VFD-fed motors, older insulation systems |
Four Steps to Start Predicting Motor Failures from Current Data
You do not need a condition monitoring consultant or a six-month implementation project. If you have 12+ months of motor data and 50+ critical motors, you have enough data to identify actionable failure patterns within your first 60 days on Oxmaint.
Collect current signals from your existing motor protection relays, VFDs, or portable data collectors. For critical motors, establish a baseline spectrum during normal operation. Oxmaint accepts standard data formats including CSV, WAV, and NumPy arrays [citation:2].
Oxmaint performs FFT and PSD analysis to establish baseline spectra for each motor. The baseline represents the healthy motor signature — all future comparisons reference this baseline to detect changes in harmonic content and sideband amplitudes [citation:2].
Review the fault detection dashboard for your top 10 motors by criticality. Identify which motors show sideband amplitudes exceeding thresholds for broken rotor bars, bearing defects, stator shorts, or eccentricity. Most steel plants identify 4-6 high-risk motors within the first two weeks of analysis [citation:3].
For each identified fault pattern, configure Oxmaint to generate preventive work orders when severity thresholds are reached. Set triggers for incipient, moderate, and severe classifications. Attach supporting spectral data and fault analysis to each work order. From this point forward, every new motor data point feeds the prediction engine — making it more accurate with every measurement [citation:1][citation:2].
ROI of MCSA-Based Predictive Maintenance for Steel Plant Motors
Planned motor repair costs 40-60% less than unplanned replacement — eliminating emergency sourcing, expedited shipping, and overtime labor [citation:3]
MCSA detects fault signatures 2-8 weeks before catastrophic failure occurs — enabling planned maintenance during scheduled outages [citation:1]
Preventing unplanned motor failure eliminates the 6-48 hours of production downtime typically required for emergency replacement
The predictive maintenance program pays for itself within 6 months through avoided motor replacements and eliminated production downtime
Frequently Asked Questions
What is Motor Current Signature Analysis and how does it work?+
What types of motor faults can MCSA detect in steel plants?+
Does MCSA require special sensors or equipment installation?+
How much data do I need to start MCSA-based predictive maintenance?+
Your Next Motor Failure Is Already in Your Current Data — Find It Before It Shuts Down Your Mill
Every current waveform your steel plant's motors have ever generated contains a piece of the pattern that predicts the next failure. Oxmaint's motor condition monitoring module collects current data correctly, analyzes it for spectral patterns, and generates the predictive work orders that keep your rolling mills running. No new sensors. No condition monitoring consultants. Import your data, identify your fault patterns, and start predicting motor failures in your first 60 days.