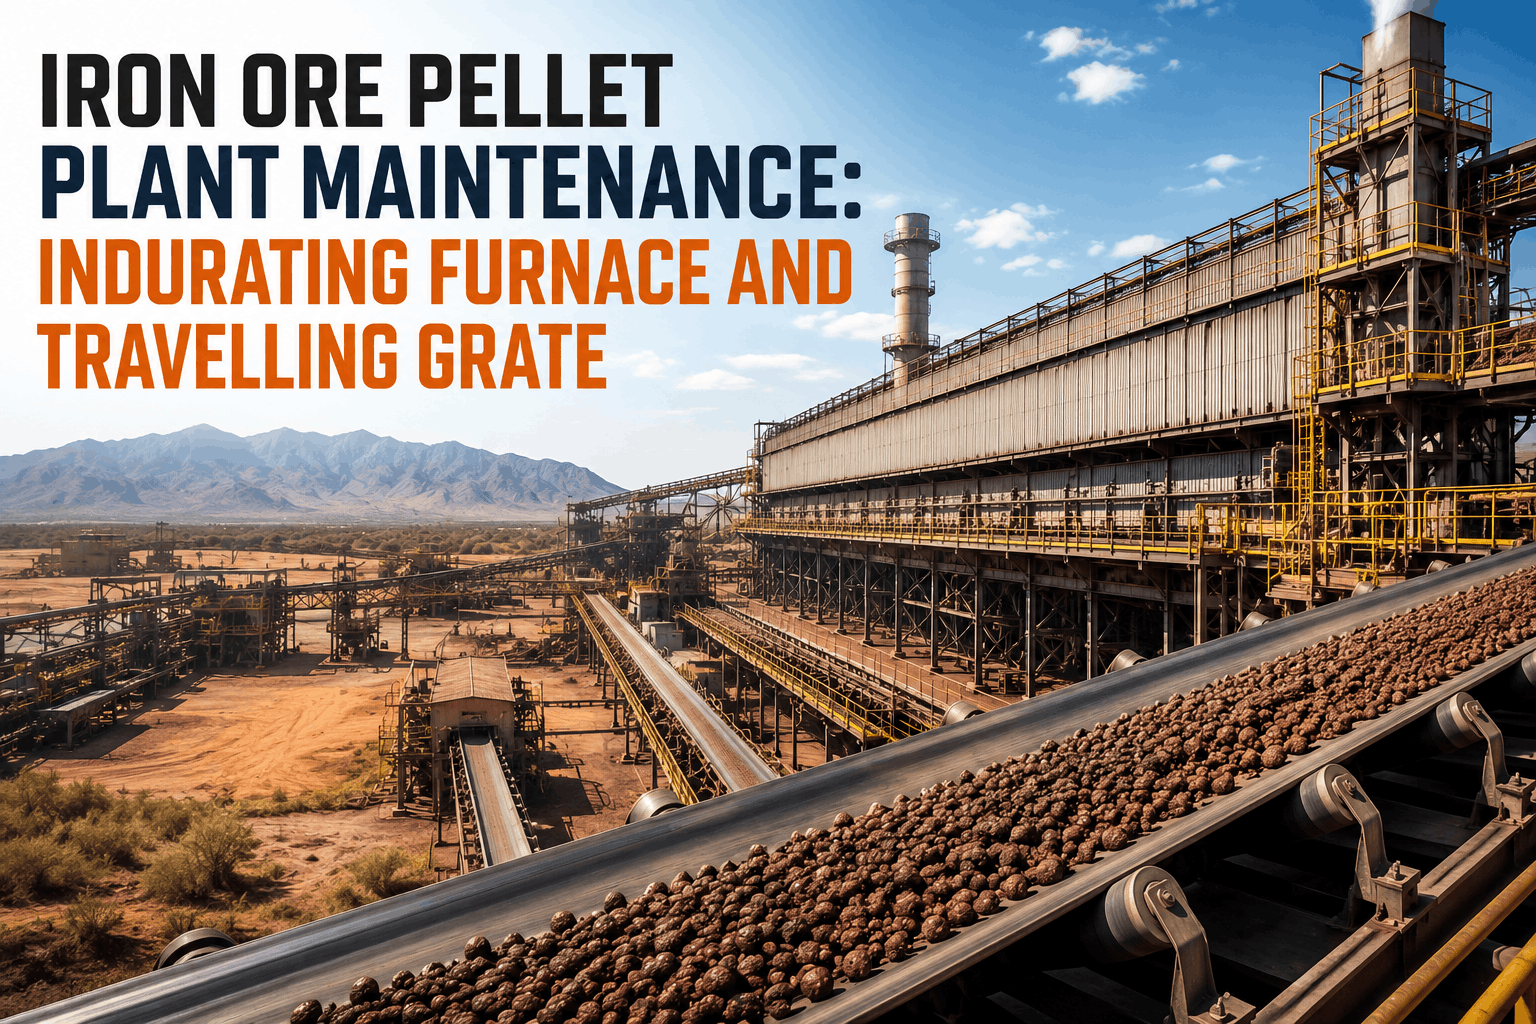
Iron ore pellet plants transform iron ore fines into hard, porous agglomerates — essential feedstock for both blast furnaces (producing hot metal for steelmaking) and direct reduction iron (DRI) plants (producing steel via electric arc furnace). Global pellet production exceeds 400 million tons annually, with 150+ dedicated pellet plants operating continuously across North America, Europe, Australia, and Asia. The straight-grate indurating furnace — the thermal heart of the process — operates at 1,300–1,350°C across three distinct thermal zones: a drying zone (0–900°C) removing moisture from green pellets, a firing/induration zone (900–1,350°C) sintering pellets into hard spheres, and a cooling zone bringing pellets back to handling temperature. A traveling grate machine carries pellets through all zones at speeds of 1.5–4.0 meters per minute, completing a full cycle every 3–4 hours. This means the indurating furnace runs 6,000+ cycles per year, with pallet cars, grate bars, and all supporting equipment cycling through extreme thermal and mechanical stress continuously. Most pellet plants operate with reactive maintenance on refractory linings, burner nozzles, and grate bar systems — replacing components only after visible damage appears. This approach creates production instability, quality variance, and accelerated wear cascading through the system. This guide explores the four critical subsystems that determine indurating furnace reliability, the condition monitoring approaches that enable predictive maintenance, and how Oxmaint delivers the operational intelligence that keeps pellet plants running at nameplate capacity while extending equipment life 20–30%.
Straight-Grate Indurating Furnace — Process & Equipment Overview
The straight-grate furnace consists of a single traveling grate machine 60–100 meters long and 4–6 meters wide, configured with three functional zones: a drying section where ignition gas burners at 900°C remove moisture from green (unfired) pellets; a firing section where 11–20 burners operating at 1,350°C sinter pellets together, developing mechanical strength; and a cooling section where water sprays cool pellets from 1,100°C back to 80–150°C for handling. The hearth layer — a 50–150 mm deep bed of previously fired pellets on the grate surface — protects grate bars from direct contact with the 1,300°C furnace atmosphere and improves heat transfer to raw pellets. Air sealing and flow distribution occur through wind boxes beneath the grate; false air suction (leakage through worn pallet seals or refractory cracks) reduces process efficiency and introduces oxygen that degrades furnace chemistry control. A complete thermal cycle requires 3–4 hours; the grate moves continuously, advancing new pellets into the drying zone as fired pellets exit the cooler. This continuous operation means equipment operates 8,000+ hours per year with essentially no breaks, creating cumulative wear on pallet cars, grate bars, grate drive chain, and burner nozzles. Understanding which equipment components limit overall furnace availability — and predicting their failure before sudden breakdowns — is the operational foundation of modern pellet plant management.
Four Critical Subsystems — Interconnected Performance
Pallet cars — typically 80–150 units per furnace — transport pellets through all thermal zones. Grate bars (40–60 mm wide, 10–15 mm thick) support the pellet bed while allowing air passage. Bars oxidize and corrode at 1,300°C, losing 2–4 mm thickness per year. Pallet wheels cycle 8,000+ times per year, with bearing wear and flange rounding limiting service life to 4–7 years. Monitoring bar thickness, wheel condition, and chain elongation enables planned replacement 2–3 weeks in advance.
Ignition and firing burners inject natural gas or oil at high pressure, achieving combustion at 1,100–1,350°C. Burner nozzles experience thermal cycling stress and ash accumulation, reducing fuel atomization and combustion efficiency. Refractory linings protect furnace walls and burner blocks; spalling linings create hot spots and allow heat loss. Temperature measurement at 20+ points enables identification of burner degradation and refractory damage 1–2 weeks before productivity loss appears.
Ceramic brick or fiber linings protect furnace structure from 1,300°C exposure. The hearth layer (previously fired pellets) serves as thermal insulation and gas distribution medium. Lining spalling reduces thermal protection and creates local hot spots; hearth layer degradation increases thermal cycling of grate bars and reduces heat transfer efficiency. Visual inspections every 500 hours and thermal imaging identify degradation 2–4 weeks before productivity impact.
Wind boxes beneath the grate distribute process air — drying in the drying zone, combustion support in the firing zone. Pallet seal degradation creates false air suction; air leakage reduces draft efficiency and destabilizes furnace draft balance. Damper control systems regulate air distribution per zone. Monitoring pressure differential, leakage rate, and damper operation enables detection of seal degradation 1–2 weeks before pellet quality variance appears.
Quality-Driven Maintenance — Mechanical Strength & Thermal Profile Control
Pellet plant maintenance is ultimately driven by product quality requirements. Mechanical strength (typically >200 Newtons per pellet for blast furnace grade) depends on complete induration — heating every pellet from center to surface to the bonding temperature of 1,200°C+. Inadequate furnace temperature, short residence time (from grate speed too fast), or uneven heating from burner degradation all produce soft pellets that fail drop-test specifications. Furnace capacity and thermal efficiency are measured by tons of pellets produced per ton of fuel burned — typically 6–8 tons pellets per ton natural gas. Burner degradation (reduced combustion efficiency from nozzle fouling) or refractory spalling (allowing heat loss through furnace walls) both reduce efficiency, requiring higher fuel rates to maintain temperature and capacity. By monitoring fuel consumption per ton produced, temperature distribution across the furnace, and end-product mechanical strength, Oxmaint detects equipment degradation that would otherwise remain hidden until product quality fails. A 3–5% rise in fuel consumption paired with pellet strength decline of 5–8% indicates burner or refractory issues; correlation of this data against time-stamped burner nozzle condition checks and refractory inspection records enables root-cause identification within days rather than weeks of troubleshooting.
Pellet Plant Condition Monitoring — Practical Measurement Approach
Oxmaint Pellet Plant Intelligence — Equipment & Quality Integration
Multi-zone temperature monitoring identifies burner degradation, refractory spalling, and process air leakage. Temperature variance alerts trigger burner maintenance or refractory inspection 1–2 weeks before productivity loss appears.
Individual pallet condition aggregates grate bar thickness, wheel wear, bearing temperature, and seal integrity. Pallets approaching multi-component failure are clustered for simultaneous overhaul, optimizing maintenance labor efficiency.
Fuel consumption trending paired with pellet mechanical strength measurement identifies which equipment degradation produces quality loss. Rising fuel consumption + declining strength = burner/refractory issue vs. rising consumption without quality impact = other thermal losses.
Oxmaint generates maintenance schedules 4–8 weeks in advance, clustering related work (pallet overhauls + burner maintenance + refractory inspections) into single furnace shutdown events, reducing annual downtime 15–20%.
Frequently Asked Questions — Pellet Plant Equipment & Maintenance
"Oxmaint's pallet car lifecycle tracking identified that Pallet 8's grate bars, wheels, and bearings were all approaching end-of-life within 3 weeks. Rather than replacing components reactively over months, we scheduled a complete pallet overhaul in a single 8-hour shutdown. The consolidated labor saved us $8K and eliminated the production disruption that would have occurred from three separate failures."
— Maintenance Director, Pellet Plant, USA · 2025
Monitor pallet cars, grate bars, burners, and refractory systems — schedule maintenance weeks in advance and extend equipment life 20–30%.