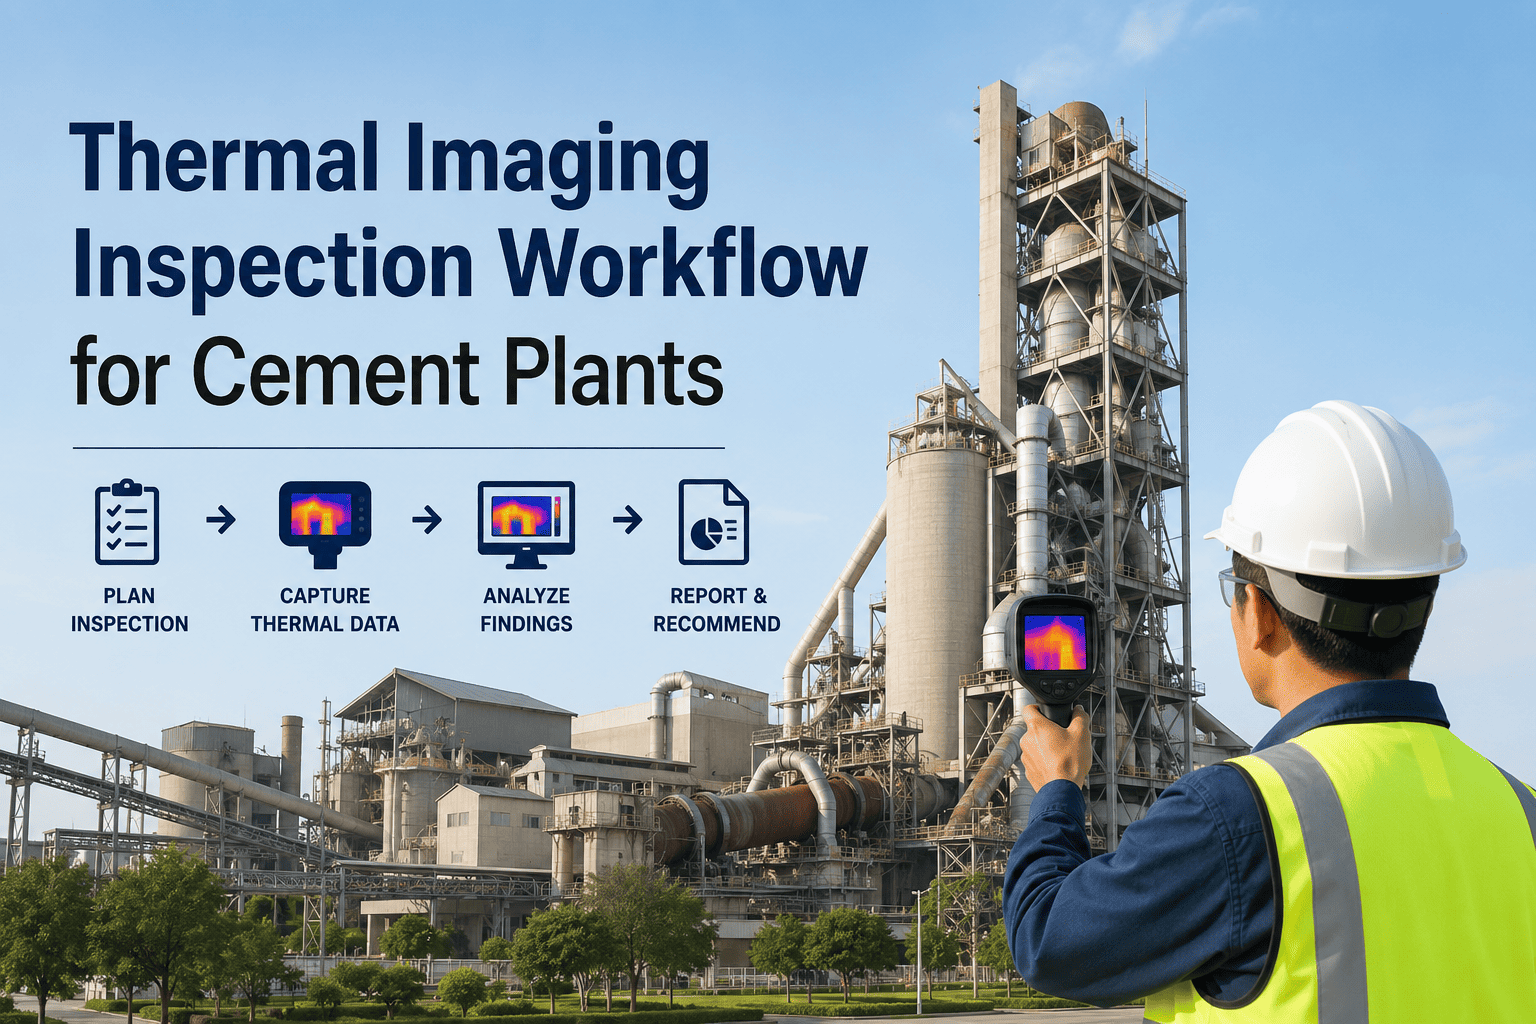
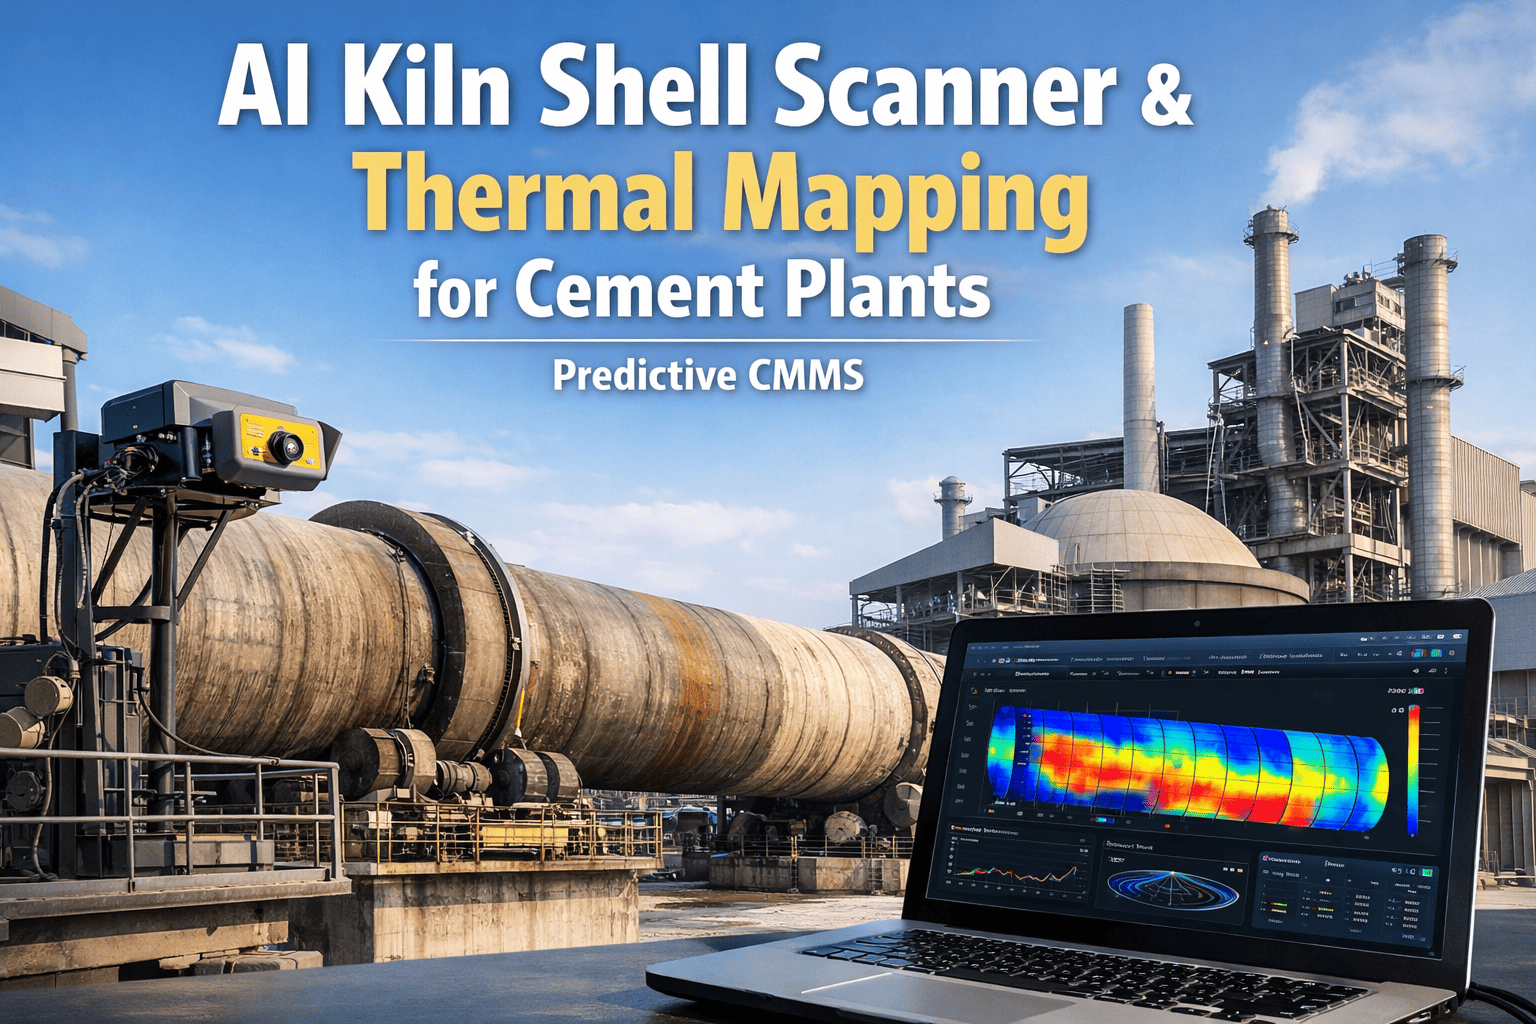
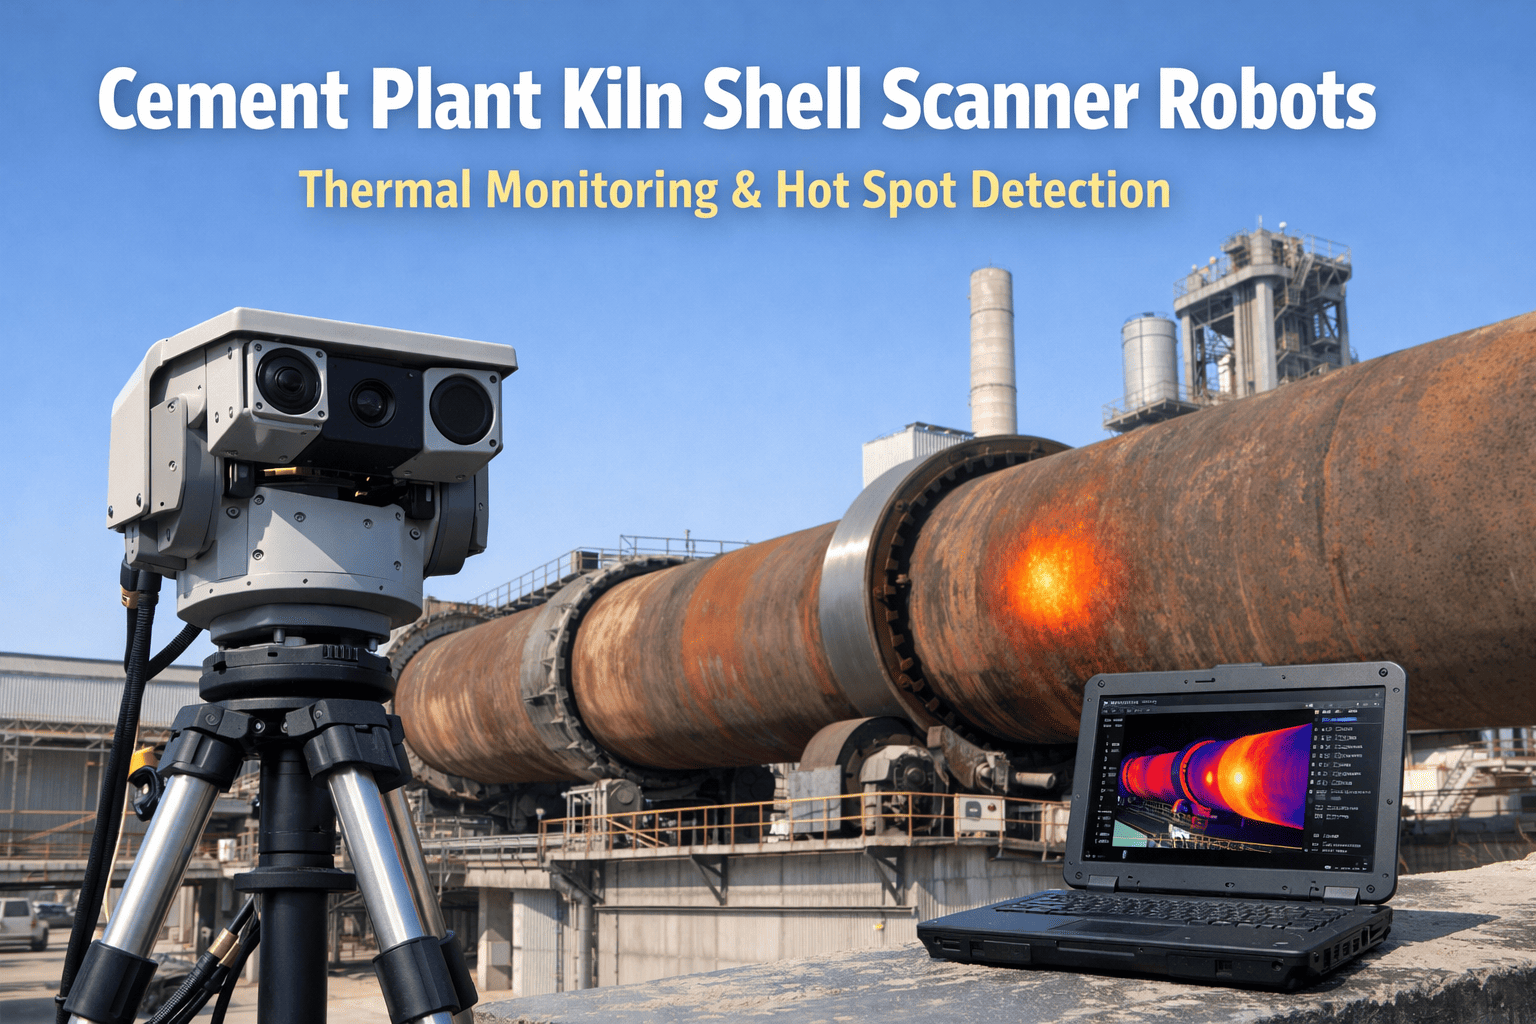
Thermal imaging inspection in a cement plant catches what vibration, oil analysis and ultrasound cannot — the refractory thinning inside a rotating kiln, the loose lug inside a 415 V switchgear cubicle, the overgreased bearing about to seize on a mill fan. A two-minute thermography scan routinely surfaces defects that would otherwise announce themselves as an unplanned shutdown, a kiln shell warp or a switchgear fire. This guide maps a complete thermal route for cement operations — cadence, targets, interpretation thresholds and the CMMS documentation that converts a quarterly walk-around into a scheduled reliability program. Start your own route in the Oxmaint CMMS with a Start Free Trial, or read on for the full inspection playbook.
THERMOGRAPHY ROUTE GUIDE
What if a single scan could catch the next kiln shell hotspot before it cost you $180,000 in unscheduled downtime?
Cement plants lose an average of 18–24 production hours per thermal-driven failure event. A disciplined infrared route across kiln shells, electrical switchgear and motor terminals finds 80% of those defects weeks before failure — and schedules the fix inside the CMMS during a planned window.
SCAN CADENCE BY ASSET TIER
A two-tier thermal route that fits a 7-day cement production cycle
Most cement reliability teams under-scan — they walk the kiln monthly and the switchgear annually, missing the 2–3 week failure signature of electrical connections. The cadence below is calibrated to a typical 1.2 MTPA plant running 330 days/year.
Kiln shell & critical drives
Scan the full kiln shell at the same tire positions every Monday morning, capturing a thermal strip map. Add the preheater cyclone cowls, clinker cooler grate and the main mill gearbox. A 40 °C rise at any shell zone above the rolling baseline triggers a refractory inspection work order.
Electrical, motors & bearings
Walk every MV/LV switchgear cubicle, motor control center, transformer bushings and the top 20 motor terminal boxes. Capture each connection under normal load (above 40% rated current). Tier 2 catches the slow-rise lug overheats that vibration and oil analysis will never see.
KILN SHELL THERMOGRAPHY
Reading the shell: five thermal zones that dictate refractory life
A kiln shell is a 60–90 meter thermal canvas. Each zone tells a different story about the brick behind it, and a 10 °C shift at the burning zone often means a 200 °C shift at the hot face of the refractory. Here is how a trained thermographer reads the strip.
Burning zone — 0 to 8 m from discharge
Target shell temperature 280–340 °C. Any reading above 380 °C signals brick thickness under 80 mm — schedule a brick condition assessment within 7 days. A localized hotspot above 450 °C is a red-brick condition: plan a controlled stop within 48 hours to avoid shell ovality damage.
ceiling
Transition zone — 8 to 30 m
Expect 240–300 °C. Coating instability here produces migrating hotspots 3–5 m wide. Track them weekly — a hotspot that holds the same kiln position for three consecutive scans indicates coating loss, not a process swing, and the brick underneath is degrading.
ceiling
Calcining zone — 30 to 50 m
Normal range 200–260 °C. This zone carries the heaviest coating. A sudden 30 °C drop on the strip map often means coating collapse and a thermal shock risk to the brick — combine the IR data with kiln torque trends before adjusting feed.
ceiling
Tire & support roller stations
Scan tire contact faces and roller journals. A roller surface reading 15 °C above its sibling on the same pier indicates bearing distress or alignment drift — the bearing will fail within 60–90 days if left untreated. Lubricant film breakdown shows as a distinct thermal crescent on the roller face.
delta
Kiln hood & cooler throat
Read castable lining temperature on the hood arch. Anything above 280 °C on the outer hood plate means the castable has spalled. This is the highest-risk shutdown zone in the plant — every unplanned hood repair costs 14–22 hours of lost clinker production.
ceiling
"On a 4-stage preheater kiln, a single uncaught burning-zone hotspot typically escalates to a shell warp within 6 weeks — turning a $14K brick repair into a $310K shell and tire realignment project."
— Worked example from a 2,800 TPD plant in the GCC region, Q3 reliability review
ELECTRICAL THERMOGRAPHY
Switchgear, motor terminals and the connections that quietly fail
Electrical faults are the second-largest cause of unplanned cement downtime after refractory. Infrared finds them at the connection point — before the lug melts, before the breaker trips, before the arc flash. Use these severity bands to triage what you scan.
| Severity band | ΔT above reference | Typical defect found | Recommended action |
|---|---|---|---|
| PRIORITY 1 | > 40 °C | Loose lug, corroded busbar joint, failing breaker pole — imminent failure | De-energize and repair within 24 hrs; treat as safety hazard |
| PRIORITY 2 | 20–40 °C | Overloaded conductor, degraded contact, undersized fuse clip | Schedule corrective WO in next 7-day planned outage window |
| PRIORITY 3 | 10–20 °C | Early oxidation, minor torque drift, normal load imbalance | Log in CMMS, re-scan in 30 days, trend the delta |
| BASELINE | < 10 °C | Normal operating thermal signature under load | No action — record as baseline reference image |
MV switchgear cubicles
Scan vacuum and SF6 breaker terminations, PT/CT secondary wiring and busbar splice joints. Load must be above 40% rated current — a cold scan is a wasted scan. Compare phase-to-phase; a 15 °C imbalance on one phase is the single most reliable predictor of a loose stator connection downstream.
Motor control centers
Image every contactor, overload relay and breaker feed. A contactor running 25 °C above its neighbors has worn main contacts — a 200-hour remaining-life signature. Replace at the next planned stop, not when the mill trips at 2 a.m.
Motor terminal boxes
Open every terminal box on the top-20 critical motors monthly. The connection strip is where vibration loosens lugs over time. A 30 °C hotspot on a single phase will melt insulation within 90 days — and the motor will short to ground.
Transformer bushings & coolers
Image HV/LV bushing connections and radiator block zones. A bushing connector 20 °C above oil temperature indicates a failing gasket or internal connection — combine with dissolved gas analysis for a full picture. Blocked cooler fins show as cold patches on the radiator.
CMMS DOCUMENTATION
Turning thermal scans into a scheduled reliability program
A thermal image without a CMMS work order is just a picture. The value of thermography is unlocked when every scan becomes a traceable record, every anomaly becomes a triggered task, and every trend becomes a decision. Here is how a cement plant builds that loop in Oxmaint.
Build the thermal route
Create a CMMS route listing every scan target — asset, position code, scan tier, reference baseline image and pass/fail ΔT threshold. The route becomes a recurring work order: weekly for Tier 1, monthly for Tier 2.
Capture in the field
The thermographer opens the WO on a tablet, scans each asset in order, attaches the IR image and tags the hotspot with a ΔT reading. No paper, no spreadsheets, no transcription errors back at the office.
Auto-trigger corrective WOs
A ΔT above the asset's priority threshold automatically spawns a corrective work order, routed to the right trade with the IR image, the baseline reference and the recommended action pre-filled.
Trend & close the loop
Each asset's thermal history stacks in the CMMS asset record. Reliability engineers trend ΔT over months to verify a repair held, justify a capital refurb or escalate to a shutdown recommendation — all from one dashboard.
WORKED EXAMPLE
A 180-asset plant, a $42K program, and the shutdown that didn't happen
Consider a single-line 1.2 MTPA cement plant with 180 thermography targets across the kiln, cooler, mills and electrical distribution. The reliability lead runs a weekly Tier 1 route (12 assets) and a monthly Tier 2 route (168 assets). Labor, camera amortization and CMMS software total $42,000 per year.
Reactive — wait for the trip
- Kiln burning-zone hotspot goes unnoticed for 6 weeks
- Shell warps; tire realignment + refractory rebuild = $310K
- 22 hours lost production at $11K/hr = $242K
- MCC contactor fails at 02:14 on a Sunday = 9 hrs downtime
- Annual exposure: $468K+
Predictive — fix in planned window
- Monday scan flags 60 °C ΔT at tire #2 journal bearing
- Corrective WO auto-spawns; bearing re-lubed at next 8-hr stop
- Burning-zone IR strip catches brick thinning at 92 mm — 14 days early
- Brick replaced in planned 24-hr stop, no shell damage
- Annual cost: $42K program · $0 unplanned
SIMPLE PAYBACK CALCULATION
Payback (months) = (Annual program cost) ÷ (Avoided unplanned loss ÷ 12)
$42,000 ÷ ($468,000 ÷ 12) = 1.08 months to break even on the thermography program
BUILD YOUR THERMAL ROUTE TODAY
Stop discovering thermal defects during the outage report
Stand up a weekly kiln shell route and a monthly electrical route in Oxmaint in under an afternoon — baseline images, ΔT thresholds, auto-triggered work orders and trend dashboards included.
FAQ
Thermal imaging inspection in cement plants — answered
How often should a cement plant scan its kiln shell with thermal imaging?
A weekly strip-map scan of the full kiln shell is the industry standard for continuous-process cement plants. The burning zone and tire stations should be imaged every Monday at the same positions, so the baseline comparison is meaningful. Critical electrical assets in the MCC and MV switchgear follow a monthly cadence — long enough to catch trending defects, short enough to act before failure. You can configure both cadences as recurring routes in the Oxmaint CMMS — start your free trial here.
What temperature delta indicates a refractory hotspot that needs action?
On the kiln shell, any localized reading exceeding 380 °C at the burning zone or 300 °C at the transition zone warrants a refractory inspection work order within 7 days. A reading above 450 °C at the burning zone is a red-brick condition — plan a controlled stop within 48 hours. Always compare against the asset's rolling baseline, not a generic spec sheet, because shell temperature depends on kiln loading and secondary air temperature.
Can thermal imaging replace vibration analysis for motors and drives?
No — the two technologies are complementary, not substitutes. Thermography catches electrical connection faults, lubrication starvation and bearing friction that vibration sensors miss early on. Vibration catches imbalance, misalignment and gear mesh defects that thermal imaging cannot see until secondary heating develops. A mature cement reliability program runs both on the top-20 critical motors, with thermal monthly and vibration monthly or continuous.
What emissivity setting should I use for a kiln shell scan?
A weathered steel kiln shell typically has an emissivity of 0.85–0.92. Set the camera to 0.90 and apply a strip of high-emissivity paint (0.95) tape at each scan reference position for calibration cross-check. Never trust an uncorrected reading on shiny stainless cladding or freshly painted surfaces — emissivity errors of 30–50 °C are common and can mask a genuine hotspot. Document the emissivity setting in the CMMS asset record so every thermographer uses the same value.
How does a CMMS turn thermal scans into a scheduled reliability program?
The CMMS converts each thermal route into a recurring work order, attaches the IR image and ΔT reading to the asset record, and auto-spawns a corrective work order when a reading crosses the asset's priority threshold. Over months, the stacked thermal history lets reliability engineers trend degradation, verify repairs held and justify shutdown timing. To see this loop configured for a cement plant, book a 30-minute demo with the Oxmaint team.
READY TO SCAN?
Your next kiln hotspot is already forming. Catch it Monday.
Deploy a complete thermal imaging inspection program across your cement plant — kiln shell, electrical switchgear, motor terminals — with routes, baselines, auto-triggered work orders and trend dashboards built into Oxmaint.
Free 14-day trial · No credit card required