Cement kiln heat balance is where maintenance discipline meets fuel economics — every percentage point of false air, every missing millimeter of refractory, and every misaligned burner tip shows up directly as specific heat consumption on your monthly fuel bill. A modern 5-stage preheater kiln operating near 3,100 kJ/kg clinker can drift to 3,500 kJ/kg or worse within months when seal maintenance, shell-coating management, and combustion tuning slip through the cracks of a reactive work-order system. Treating thermal efficiency as a maintenance KPI — not just a process metric — is what separates plants that sustain 92%+ kiln uptime from those fighting quarterly energy variances. The framework below maps the heat-balance levers a maintenance team actually controls, with benchmarks, inspection intervals, and a CMMS workflow you can deploy this quarter. Start Free Trial to turn these checks into scheduled, auditable work orders.
Can your kiln hold its design heat rate — or is 300 kJ/kg of clinker quietly leaking out every cycle?
False air, refractory thinning, and uncalibrated combustion together drive 8–12% of avoidable fuel cost in most cement plants. A CMMS-led heat-balance program brings specific heat consumption back toward design — and keeps it there.
Where the heat goes — and what maintenance actually controls
A typical dry-process kiln heat balance distributes roughly 3,100 kJ/kg of clinker across four broad buckets. Process engineers tune the chemistry and the burning zone; maintenance teams own the integrity of the seals, lining, insulation, and combustion hardware that determine whether the plant stays near those numbers month after month.
Clinker formation heat
Endothermic calcination and sintering. This is the thermodynamic floor — maintenance can't change the chemistry, but stable kiln operation protects the specific heat rate by avoiding thermal cycling that degrades the lining.
Preheater & exhaust gas loss
Fals-air ingress through stage doors and seals dilutes exhaust, lowers efficiency, and raises fan load — directly controllable by maintenance.
Shell radiation & convection
Driven by refractory thickness and coating stability. Each 50 mm of lost brick adds measurable shell temperature and kiln fuel demand.
Cooler & clinker discharge
Secondary-air recovery depends on cooler refractory, grate condition, and seal integrity. Maintenance gaps here steal combustion air preheat.
Unaccounted & measurement drift
The residual. When it grows beyond 3%, suspect false-air leaks, fouled sampling lines, or failing flow meters — all maintenance-owned.
False air is the cheapest energy leak to fix — and the most ignored
Every 1% of false air in the preheater raises specific heat consumption by roughly 8–10 kJ/kg and increases ID-fan power by 2–3%. On a 5,000 tpd kiln, a 5% false-air overrun translates to roughly 4,600 GJ of wasted fuel per year — six-figure dollars that maintenance, not process, recovers.
Kiln inlet & outlet seals
Segmented spring-loaded or pneumatic seals wear at 8–12 mm per 1,000 operating hours. Inspect every 30 days under planned downtime; replace leaf segments before gap exceeds 5 mm. A 10 mm radial gap at the inlet can pull 3–4% false air.
Preheater stage inspection doors & poke holes
Worn gaskets and deformed door frames are the dominant false-air source on most 4- and 5-stage towers. Re-gasket during every scheduled shutdown; verify frame flatness within 1 mm. Tag every door with a QR-coded CMMS inspection point.
Tertiary air duct expansion joints
Fabric and metal bellows fail under cyclic thermal stress. Monitor for hot spots weekly with a thermal imaging survey; plan replacement at 18–24 months regardless of visible condition, before rupture forces an unplanned 12-hour outage.
Kiln hood & cooler seals
Hood-to-cooler seals govern secondary air recovery. A compromised seal lets cold tramp air dilute 950 °C secondary air, dropping it 80–120 °C and forcing the burner to consume more fuel to reach the same burning-zone temperature.
A 5,000 tpd kiln with 5% preheater false air, 320 operating days, and $9/GJ fuel loses roughly $215,000 per year — recoverable through a seal and gasket program costing under $35,000 installed. Payback inside the same fiscal quarter.
Coating stability and brick thickness — the thermal armor you maintain
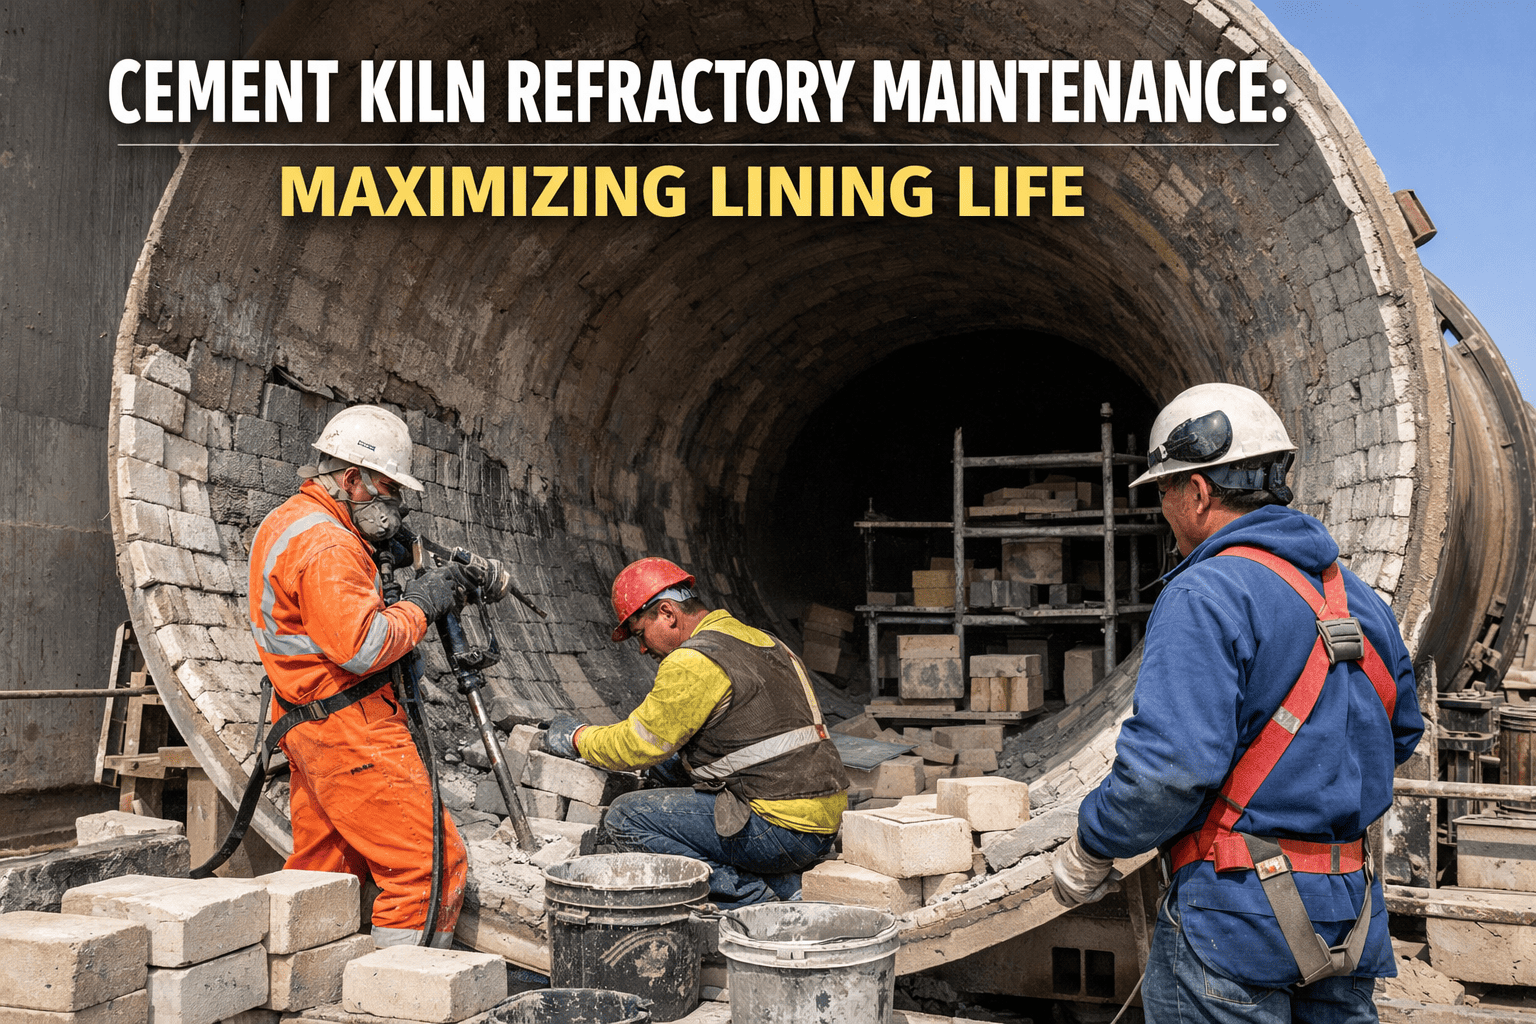
Refractory is not just a wear item; it is the thermal boundary that sets shell loss. Shell temperature above 330 °C in the burning zone signals brick thickness below 100 mm — and every additional 10 °C of shell rise costs roughly 4–6 kJ/kg in extra radiation. A CMMS-driven thickness-tracking program catches the drift before it becomes a hot spot.
Shell thermography survey
- Walk the kiln with a thermal camera at consistent load and speed.
- Log shell temperature every 2 meters against the brick-zone map in the CMMS asset register.
- Flag any zone trending +20 °C above its three-month rolling average.
- Photograph hot spots and attach to the kiln asset record for shutdown planning.
Brick thickness measurement
- Laser-profile the lining at 1-meter intervals in the burning zone, transition zone, and lower preheater riser.
- Record residual thickness against original spec; plan gunning or replacement below 120 mm.
- Inspect anchors and castable in the inlet cone and tertiary air take-off for spalling.
- Update the refractory lifecycle forecast in the CMMS to trigger next planned relining.
Coating & feed-ring inspection
- Inspect through the burner pipe viewport; note coating ring height and stability.
- Coordinate with process on raw-mix sulfur, alkali, and silica-modulus trends that affect coating.
- Verify feed-end scoop and splash plate condition — asymmetry destabilizes coating and heat distribution.
- Record observations in a structured CMMS checklist to build a coating-stability history.
Insulation & backup lining audit
- Audit preheater cyclone and duct insulation thickness; replace compacted ceramic fiber.
- Check calciner and riser duct backup lining for shrinkage gaps at expansion joints.
- Verify cooler tertiary air duct insulation integrity with spot thermography.
- Schedule findings into the next planned shutdown work scope in the CMMS planner.
Burner, cooler, and combustion hardware — the maintenance side of the flame
Combustion tuning is usually treated as a process-engineering task, but the physical condition of the burner pipe, primary-air fan, and cooler grate determines whether tuning even holds. A misaligned burner tip by 15 mm shifts the flame 0.5 m down the kiln, raises shell temperature locally, and shortens brick life by weeks.
| Combustion asset | Maintenance task | Interval | Energy impact if skipped |
|---|---|---|---|
| Burner pipe & nozzle | Internal cleaning, tip-wear gauging, alignment check to kiln axis | Every shutdown (8–12 wk) | Flame shift, CO rise, +20–40 kJ/kg |
| Primary air fan | Vibration analysis, impeller inspection, inlet-vane calibration | 30 days / 90 days | Primary-air ratio drift, incomplete combustion |
| Cooler grate & hydraulic drive | Grate-plate wear check, stroke calibration, seal-strip replacement | 60 days / shutdown | Secondary-air loss, clinker discharge temperature rise |
| ID fan & preheater fan | Performance curve test, blade erosion inspection, damper calibration | 90 days | Excess draft or starvation, false-air masking |
| Gas analyzers & sampling lines | Calibration with reference gas, line heat-trace and filter check | 7 days | Bad O₂ / CO data drives wrong combustion decisions |
A plant that fixes its analyzer sampling lines, re-seals the preheater doors, and re-gauges the burner tip at every shutdown typically recovers 150–220 kJ/kg inside a single operating quarter — without any process-chemistry change. That is pure maintenance ROI.
A CMMS-driven heat-balance program in four phases
Sustained thermal efficiency is not a project — it is a maintenance cycle. This 90-day rollout schedule moves a kiln from ad-hoc energy firefighting to a structured, auditable program inside a CMMS, with measurable heat-rate targets at each gate.
Establish the heat-balance baseline
- Run a full kiln heat balance with measured fuel, air, feed, and clinker data.
- Record false-air O₂ traverse at each preheater stage and the kiln backend.
- Import the kiln, preheater, cooler, and fan asset hierarchy into the CMMS.
- Set the current specific heat consumption as the baseline KPI.
Execute the false-air & seal work pack
- Generate CMMS work orders for all priority seal, gasket, and door findings.
- Replace inlet/outlet seal segments; re-gasket every preheater inspection door.
- Repair or replace any tertiary air duct expansion joint flagged in the survey.
- Re-measure false air after each work-order closure to confirm the gain.
Stabilize refractory & coating
- Complete the planned-shutdown brick thickness profile and gunning scope.
- Align and clean the burner pipe; verify nozzle wear and primary-air channels.
- Calibrate gas analyzers and clear all sampling-line blockages.
- Begin the monthly shell thermography survey cycle in the CMMS.
Lock in the efficiency gain
- Schedule recurring CMMS rounds: weekly coating, monthly thermography, quarterly insulation.
- Tie each work order to the heat-balance KPI dashboard for trend visibility.
- Hold a monthly energy-maintenance review with operations and reliability leads.
- Target: specific heat consumption within 3% of design, sustained for two consecutive months.
Turn kiln heat-balance checks into scheduled, auditable work orders
Oxmaint gives cement maintenance teams asset hierarchies, recurring rounds, KPI dashboards, and shutdown planning in one CMMS — built for the realities of a 24/7 kiln.
Cement kiln heat balance & energy maintenance — answered
How often should a cement kiln heat balance be performed?
A full measured heat balance should be run at least twice a year — typically after each major shutdown and again mid-cycle — plus immediately whenever specific heat consumption drifts more than 3% from baseline. A lighter monthly false-air O₂ traverse and shell thermography survey act as the operational pulse between full balances. Start Free Trial to schedule both as recurring CMMS rounds.
What is an acceptable false-air percentage in a preheater kiln?
A well-maintained 4- or 5-stage preheater should hold total false air below 8% at the preheater exit and below 5% at the kiln inlet. Anything above 12% signals seal, door, or expansion-joint failure that is silently inflating fuel cost. Each 1% reduction typically saves 8–10 kJ/kg of clinker and 2–3% on ID-fan power.
How does refractory thickness directly affect kiln fuel consumption?
Shell radiation and convection losses scale with shell temperature, which rises as brick wears thin. Once burning-zone brick drops below 100 mm, shell temperature typically exceeds 330 °C and every additional 10 °C adds roughly 4–6 kJ/kg. A planned relining timed from CMMS thickness tracking is almost always cheaper than the fuel penalty of running a thin lining to failure.
Can a CMMS genuinely reduce kiln specific heat consumption?
Yes — by converting heat-balance findings into scheduled, recurring work orders instead of one-off repairs. Plants that structure seal inspections, thermography, analyzer calibration, and burner alignment as CMMS rounds typically recover 150–220 kJ/kg within one operating quarter and hold the gain, because the discipline is enforced by the system rather than by individual memory. Book a Demo to see the kiln energy workflow live.
What is the single highest-ROI energy maintenance task on a kiln?
Re-sealing the preheater inspection doors and kiln inlet/outlet seals during a planned shutdown. The material cost is modest — gaskets, seal segments, and labor — yet a 5% false-air reduction on a 5,000 tpd kiln can return over $200,000 per year in fuel savings. It is the fastest, lowest-risk energy win a maintenance team owns end to end.
Defend your kiln's design heat rate — every shift, every shutdown
Schedule the seals, thermography, refractory, and combustion checks that keep specific heat consumption near 3,100 kJ/kg. Oxmaint makes it a system, not a memory exercise.
Free 14-day trial · No credit card